How Does an Airless Paint Sprayer Work? Inside the Pump That Builds the Pressure

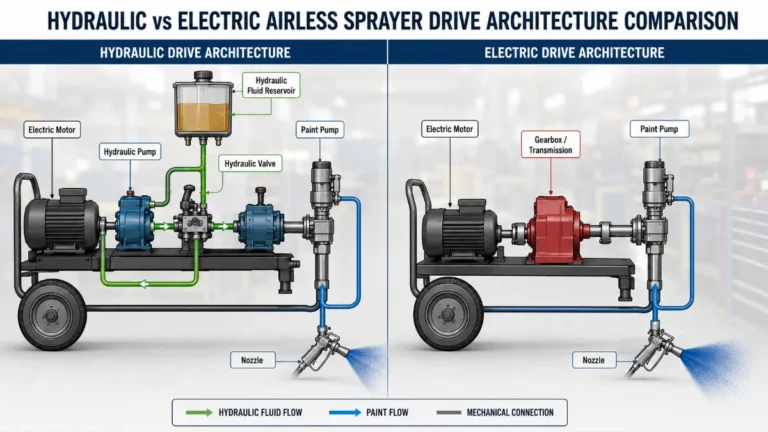
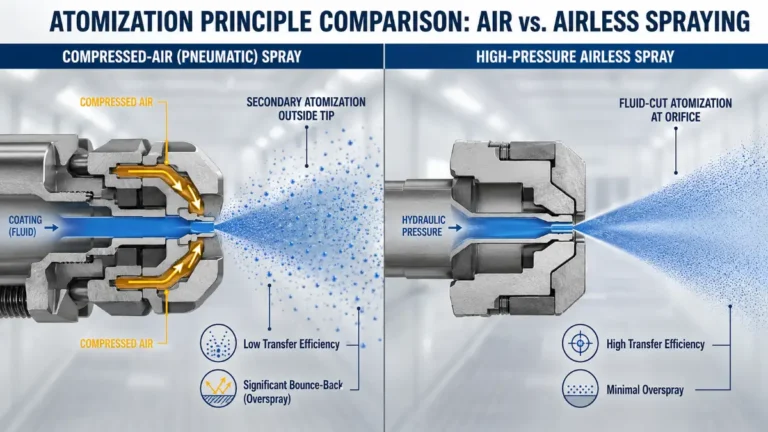
How does an airless paint sprayer work: a motor drives a piston pump that pressurizes the coating directly. The pump draws paint into the fluid section, where a plunger moving back and forth builds pressure. Check valves control the flow of coating into the hose, while the spray tip shapes the fan. Hydraulic shear at the orifice atomizes the material without compressed air.
Most explanations of how does an airless paint sprayer work focus on the pump generating high pressure, without explaining the internal components responsible for maintaining it. For contractors reviewing a quote sheet, this information alone offers little practical value. They also need to understand how pressure remains consistent, which components are most prone to wear, and how mechanical failures affect the finish. This guide examines the fluid section to address these three questions.
Why Pump Pressure Matters More Than Motor Wattage for Downtime
Quote sheets list motor wattage, flow rate, and maximum tip size, but these figures don’t show which parts inside the pump maintain pressure or how wear can affect the finish. Motor wattage alone doesn’t determine performance. Maintaining steady pressure also depends on the condition of the components inside the lower pump body.
Standard practice on the dial is simple: set the pressure to the lowest point that still gives a full, clean fan, and stop there. Past that point, extra pressure adds overspray and bounce-back, burns more coating, and wears the tip and the pump packings faster.
For buyers, the important question is not how much pressure the sprayer can produce, but how consistently it can maintain that pressure. The answer comes down to how the internal components work together.
How Does an Airless Paint Sprayer Work? The Five-Step Pressure Chain
At its core, an airless paint sprayer uses a positive-displacement piston pump to move coating through a hose and spray gun under pressure. The process can be broken down into five steps:
- The intake foot valve (inlet check valve) opens on the suction stroke, and coating is drawn from the bucket into the fluid section, also called the lower pump body.
- The piston rod changes direction and pushes against the trapped fluid, increasing pressure inside the cylinder sleeve.
- The intake valve closes while the outlet valve opens, allowing pressurized coating to flow from the pump into the high-pressure hose.
- At the spray gun, the coating passes through the tip’s fixed orifice, where hydraulic shear breaks it into fine droplets as it exits.
- The atomized coating forms a flat spray fan just beyond the orifice, with its width set by the tip number.
Tip numbering follows an industry-standard convention: the first digit times two gives the fan width in inches at a 12-inch gun distance, and the last two digits give the orifice in thousandths of an inch. A 515 throws a fan of roughly 10 inches through a .015-inch orifice.
Step four is often misunderstood. Unlike compressed-air sprayers, airless systems do not mix air with the coating during atomization. For a comparison of finish quality, overspray, and viscosity requirements, see our air vs airless paint sprayer decision guide.
Inside the Fluid Section: Every Part That Carries the Pressure

Each component in the lower pump body plays a specific role in maintaining pressure. Start from the right-hand column: find the symptom you see, then check the part it points to.
| Component | Job in the pressure chain | Symptom that points here |
|---|---|---|
| Intake foot valve (inlet check valve): ball on a tungsten-steel valve seat | Opens on the suction stroke, then seals to trap fluid for the pressure stroke | Pump struggles to prime, or keeps cycling with the gun closed |
| Outlet valve: ball on a tungsten-steel valve seat | Seals during suction, lifts to pass fluid up the line on the pressure stroke | Pressure sags between strokes; fan surges and thins in rhythm with the pump |
| Piston rod | Reciprocates in the sleeve; the moving surface that displaces the fluid | Leakage at the throat, with visible scoring on the rod |
| Cylinder sleeve / liner | Bore the rod runs in; its fit to the rod sets how much fluid can escape per stroke | Fluid past the packings on every stroke, with fresh packings already fitted |
| V-Packings (UPE & cowhide) | Seal the rod at the throat and piston so pressure stays in the fluid path | Weeping at the throat, followed by a pressure drop |
| Spray tip (tungsten carbide) | Fixed orifice that converts pressure into a sheared fan | Orifice enlarges and fan narrows; output rises while coverage falls |
Symptoms can overlap, so check the component before ordering replacement parts. Refer to your model’s service manual to determine when a part needs replacing and which components are replaced together. This table is intended to help narrow down the possible causes.
Valve balls are matched to the model: ceramic balls on the GTB-395, 595 and 920, titanium-alloy balls on the 935, and alloy balls on the 700 and 795. Seats are tungsten steel across the range. The tip is a different part in a different material — tungsten carbide.
Rod and sleeve materials follow the SKU, not the model name, and most models come in more than one version. A Dual-Ceramic Version pairs a ceramic-coated rod with a ceramic-lined cylinder sleeve (stainless shell, ceramic bore). A Single-Ceramic Version pairs a ceramic-coated rod with a stainless steel cylinder liner. A Stainless Steel Version runs a stainless steel rod in a stainless steel cylinder liner. Ask which version a quote covers.
For how the two pump architectures compare, see piston pump vs diaphragm pump.
How Does an Airless Spray Gun Work Once the Fluid Reaches It?
The spray gun controls when coating passes through the tip, rather than breaking it into droplets. A filter in the handle catches debris before it reaches the tip. Pulling the trigger lifts a needle off its seat, opening the valve so pressurized paint can pass from the hose to the tip. Releasing the trigger shuts the valve and stops the spray.
In a typical airless system, the gun filter sits between the handle and the spray tip. It is the final and finest of three filtration stages, designed to catch small particles before they reach the tip’s orifice. At the spray tip, pressurized coating passes through a carbide orifice just a few thousandths of an inch wide. As it exits, hydraulic shear breaks the liquid into fine droplets.
Other spray systems differ in how they use air. Compressed-air guns, HVLP (high volume, low pressure) turbines, and air-assisted airless (AAA) systems all feed air to the cap to break up or shape the coating. GUTUBAO does not manufacture compressed-air, HVLP, or air-assisted spraying equipment. These systems are available from other manufacturers. An airless spray gun has no separate air line. Instead, the pump supplies the pressure needed to move the coating, while the tip’s orifice breaks it into droplets. Fan width changes with the distance between the spray gun and the surface. Since tip numbers are rated at a distance of 12 inches, maintain a consistent spraying distance for even coverage.
Where the Pressure Goes Between the Pump and the Tip

Pressure can drop as the coating travels from the pump to the spray tip. Three factors can affect how much pressure reaches the orifice.
Filtration is the first factor. Typical airless filtration is staged and gets finer toward the gun: an inlet strainer at the pickup protects the pump, a manifold filter at the pump outlet protects the pistons, and the gun filter protects the tip. Higher mesh number means smaller holes and finer filtration.
Second is the hose. Its length and diameter, along with the coating’s viscosity, affect how much pressure is lost before the material reaches the spray gun. Hose rating is a separate matter: hoses of the same diameter and color can carry very different ratings, so read the W.P. printed on the hose you actually run. Never guess it from the size.
Third is the tip. A larger orifice lets more coating pass through, requiring the pump to maintain a higher flow rate. As the orifice wears and widens, the same increase in flow can occur unintentionally. For scale, airless sprayers as a category typically run roughly 1,000 to 3,300 PSI, with professional units above 4,000. These are general industry figures, so check your machine’s specification sheet for its rated pressure.
Five Ways Contractors Kill Pump Pressure
Five common practices can lead to pressure loss and premature wear on pump components.
- Increasing the pressure to compensate for a worn spray tip. As an industry rule, more pressure does not fix a worn tip. Instead, it accelerates wear on the tip, pump, and packings while increasing overspray. Replace the tip and return to the lowest pressure that gives a full fan.
- Spraying with a tip that has lost 25% of its original fan width. As a general rule, replace the spray tip once its fan width has decreased by approximately one-quarter. For example, a 515 or 517 tip that originally produced a 10-inch fan should be replaced when the width narrows to around 7.5 inches.
- Keeping the pressure set too high throughout the day. Once the optimal spraying pressure is reached, increasing it further leads to more overspray, greater paint consumption, and faster wear on the pump packings.
- Using the wrong filter mesh size or skipping a filtration stage. A filter that is too coarse can let debris reach and clog the spray tip, while one that is too fine can restrict coating flow to the gun. Filter openings must be small enough to trap particles that could otherwise cause blockages.
- Using a wire or metal pick to clear a clogged spray tip. Soak the tip in the right solvent, brush it with a soft nylon brush, and check it against the light. Metal tools scratch or chip a carbide orifice. A chipped orifice means replacing the spray tip, not cleaning it.
Dropping all five habits costs nothing; keeping them costs pressure.
The Pressure Is Real: Fluid Injection Risk and Grounding Discipline
An airless sprayer forces coating through a small metal orifice at high pressure, breaking the liquid into fine droplets. A stream at this pressure penetrates skin. NIOSH’s guidance for spray painters describes the airless paint stream as a hazard of hypodermic injection into anyone who contacts the spray, and notes the same injection can come from a tiny hose leak, not only the tip. Injected paint spreads under the skin, even through a tiny entry wound. In NIOSH’s words, such an injury “requires immediate medical attention.” For further safety guidance, refer to the NIOSH publication on spray painting practices.
Follow these two safety rules. Never aim the spray gun at yourself or another person, and never attempt to locate a leak with your hand. Anyone struck by a high-pressure spray must seek emergency medical attention immediately, however minor the injury appears. Tell the treating physician it is a high-pressure injection injury.
Safety Notice: When spraying flammable or solvent-based coatings, keep the sprayer at least 6 m (20 ft) away from areas containing explosive vapors and ventilate the area thoroughly. Remove all ignition sources. Before spraying, make sure the sprayer, hose, spray gun, and metal containers are properly grounded. Keep a fire extinguisher within reach. Review the coating’s Safety Data Sheet (SDS) before spraying. Never spray halogenated hydrocarbon solvents through the equipment. These rules apply to airless spraying equipment from any manufacturer.
How We Machine and Test That Pressure Chain in Our Own Shop

Founded in 2010, GUTUBAO manufactures all its pump bodies, motors, and printed circuit boards (PCBs) in-house, with more than 200 CNC machines supporting production.
GUTUBAO uses Brother SPEEDIO S700Z1 machining centers for pump bodies and aluminum front and back covers. During that machining operation, each part is automatically flipped so both sides are finished without removing and securing it again. This helps maintain concentricity and squareness. Connecting rods are machined on American Haas CNC machines, where both bores are cut in one setup without turning the part around. Keeping the bores parallel reduces the risk of an off-center bore scoring the cylinder.
A tolerance of ±0.01 mm is maintained on key machined metal mating surfaces. This tolerance applies only to those specific surfaces, not to every component in the equipment.
Pump core components undergo geometric and mechanical inspections, including concentricity measurements on a Carl Zeiss coordinate measuring machine (CMM) and concentricity and roundness checks using a projector. Piston rods are inspected for surface roughness, runout, and tensile strength, while bore dimensions are measured with an electronic air gauge. Additional tests cover hardness, spring force, and the leak-tightness of valve balls and seals. Each valve ball is leak-tested individually.
Each PCB is powered for a 4-hour burn-in, and each finished machine is held under continuous high-pressure load for 30 minutes before it leaves the line. All units pass through three inspection stages: first-piece, in-process, and final inspection. These checks apply to every machine, rather than a sample of the production batch.
GUTUBAO holds roughly 70% of the domestic market, and its machines ship to dozens of countries.
Choose a sprayer for your coating and your volume, not from a catalog page alone. Browse our electric airless paint sprayers to compare available models, or submit your project requirements through the RFQ form. Our engineering team can then quote a standard model or a custom configuration suited to your coatings and production volume.
FAQ
How does a paint sprayer work if there is no compressor on the machine?
An airless paint sprayer works without a compressor because its pump pressurizes the coating directly. A motor moves a plunger back and forth inside a cylinder sleeve, while check valves direct the fluid into the hose. At the spray tip, hydraulic shear breaks the pressurized coating into fine droplets, forming a spray fan. Air never touches the paint.
Can I run an airless sprayer at lower pressure without losing the fan?
Yes. Start with a low pressure setting and test the spray pattern on cardboard. Increase the pressure gradually until the fan is even, with no tails, fingers, or gaps. Stop adjusting once the pattern is consistent. Operating at the lowest pressure that produces a full spray fan helps minimize paint waste and extends the service life of the tip and pump. If the pattern remains uneven despite adjusting the pressure, check the spray tip for wear.
Why is it called “airless” — what actually atomizes the paint if not compressed air?
Hydraulic shear atomizes the paint. The pump forces the coating through a small carbide orifice at high pressure, breaking it into fine droplets as it exits the spray tip. Compressed-air and HVLP spray guns use air to atomize the coating, while air-assisted airless systems introduce air at the cap to improve the spray pattern. All three are built by other manufacturers. Unlike these systems, an airless sprayer operates without a separate compressed-air supply.
What are the main components inside an airless sprayer pump?
The fluid section contains an intake foot valve (inlet check valve) with a ball resting on a tungsten-steel valve seat, along with an outlet valve of the same design, a piston rod, and a cylinder sleeve or liner. V-packings made from UPE and cowhide provide a seal around the rod. Materials used for the valve balls, piston rod, and sleeve differ by model and version, so check the specifications before ordering replacement parts.
How do I know when the tip or the packings need replacing?
Check the spray fan to assess tip wear. Replace the tip when the fan width has narrowed by approximately 25% compared with a new tip. Reported tip life varies widely, with estimates for latex coatings ranging from roughly 15 to 135 gallons, depending on abrasiveness, operating pressure, and maintenance. These figures should be treated as a rule of thumb rather than fixed replacement intervals. For packings, look for fluid leakage around the throat followed by a drop in pressure. Verify intervals against your own coating and duty cycle on-site.